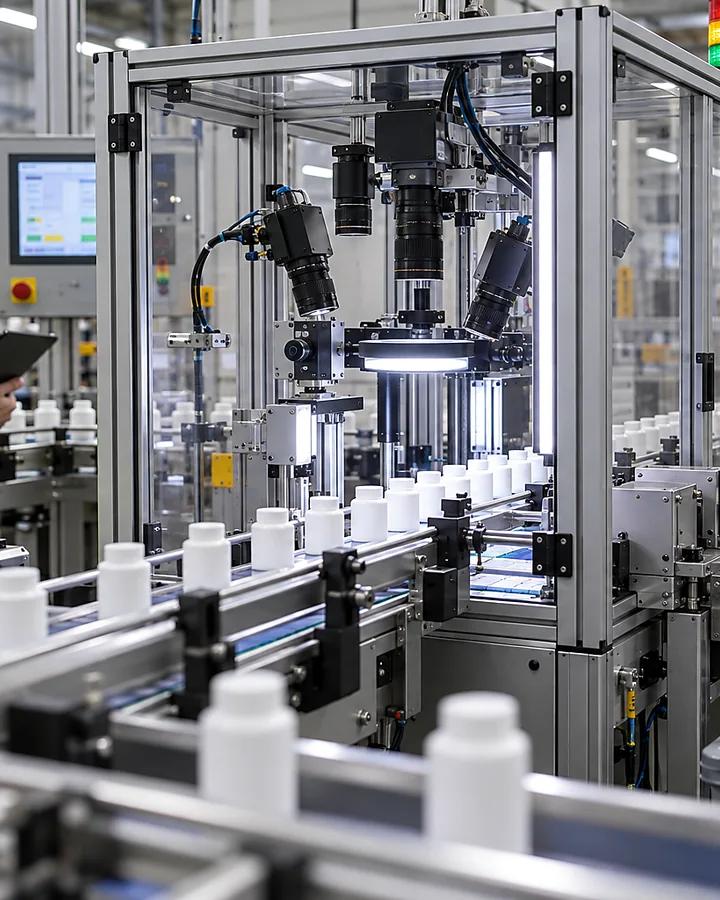
Packaged trays on a conveyor beneath clear covers beside a control screen.
Dynamic production weighing

High Speed Checkweighing

Plan high speed checkweighing around the smallest meaningful weight difference, normal product and tare variation, pack transfer, line speed, reject confirmation and traceable test evidence.

Speak directly with Oxford Vision Systems about checkweighing at high production rates.

Quick answer

How do we assess checkweighing performance at our required line speed?

State the pack dimensions, weight range and actual spacing at the highest sustained production rate. Use known challenge packs to test measurement decisions and reject tracking. Include product transfers, vibration observed at the location and consecutive rejects, then agree acceptance from the recorded trial results.

Packaged trays on a conveyor beneath clear covers beside a control screen.
Clear food containers on a blue conveyor beside a transparent cover and control screen.
Six useful questions

Describe what you need from high speed checkweighing before choosing a solution

For high-speed in-line pack weight checking, share the normal condition, realistic range and difficult cases the finished system must handle.

Question 1

Pack Weight, Stability, Spacing and Normal Tare Variation At the Required Rate

For your initial enquiry about high speed checkweighing, describe the current position, required outcome, acceptable limits and known exceptions for pack weight, stability, spacing and normal tare variation at the required rate. That lets us compare options against your real production rather than one nominal value.

Question 2

Smallest Meaningful Weight Difference and Acceptance Window

For your initial enquiry about high speed checkweighing, describe the current position, required outcome, acceptable limits and known exceptions for smallest meaningful weight difference and acceptance window. That lets us compare options against your real production rather than one nominal value.

Question 3

Pack Dimensions, Stability and Conveyor Presentation

For your initial enquiry about high speed checkweighing, describe the current position, required outcome, acceptable limits and known exceptions for pack dimensions, stability and conveyor presentation. That lets us compare options against your real production rather than one nominal value.

Question 4

Line Speed, Spacing, Vibration and Transfer Conditions

For your initial enquiry about high speed checkweighing, describe the current position, required outcome, acceptable limits and known exceptions for line speed, spacing, vibration and transfer conditions. That lets us compare options against your real production rather than one nominal value.

Question 5

Reject Device, Removal Confirmation and Reject-Bin State

For your initial enquiry about high speed checkweighing, describe the current position, required outcome, acceptable limits and known exceptions for reject device, removal confirmation and reject-bin state. That lets us compare options against your real production rather than one nominal value.

Question 6

Test Packs, Challenge Method, Records and Production Response

For your initial enquiry about high speed checkweighing, describe the current position, required outcome, acceptable limits and known exceptions for test packs, challenge method, records and production response. That lets us compare options against your real production rather than one nominal value.
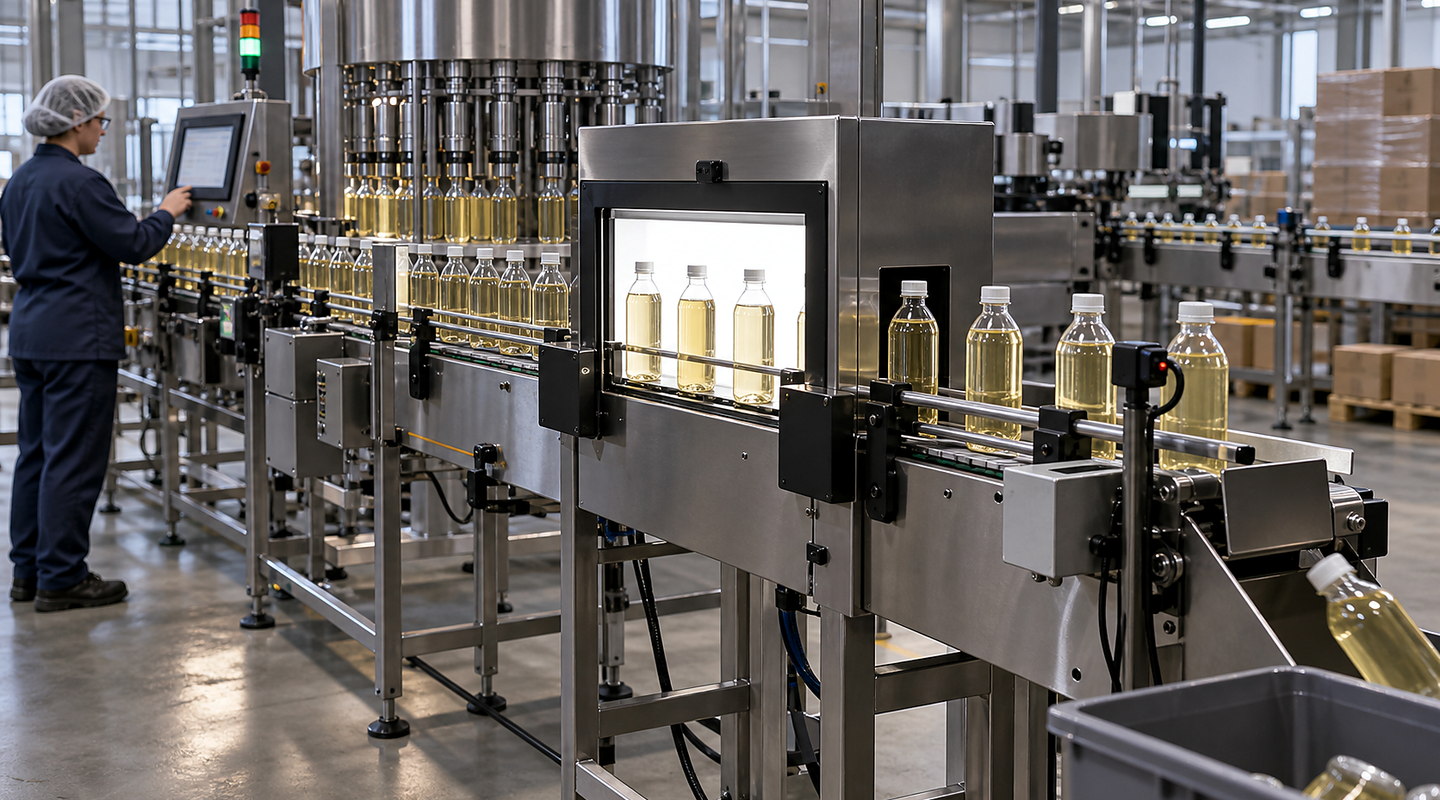
Applications

Two useful starting points for high speed checkweighing

The right choice changes with pack weight, stability, spacing and normal tare variation at the required rate, smallest meaningful weight difference and acceptance window, your line layout and required results.

What happens next

Your route from an initial enquiry to a working solution

You can review decisions about reject device, removal confirmation and reject-bin state and test packs, challenge method, records and production response at each stage.

  1. 01

    Measure Normal Product and Packaging Variation

    Share representative packs, measured weight variation and known test packs, including the normal range for pack weight, stability, spacing and normal tare variation at the required rate and the difficult smallest meaningful weight difference and acceptance window cases.

  2. 02

    Trial the Real Pack Range At Intended Line Conditions

    Compare suitable methods and use focused trials to show how each option performs against pack dimensions, stability and conveyor presentation.

  3. 03

    Integrate Transfers, Controls, Rejection and Confirmation

    Connect the equipment to your line, services and controls while resolving line speed, spacing, vibration and transfer conditions for day-to-day operation.

  4. 04

    Challenge Known Weight Faults and Retain Agreed Test Results

    Confirm reject device, removal confirmation and reject-bin state, then complete and record test packs, challenge method, records and production response before your operating team takes over.

Important limits

Know what needs a separate check

Your final solution for checkweighing at high production rates must reflect the law, current standards and site-specific risks that apply to your installation.

Application decision

High speed is a complete line condition, not one packs-per-minute figure

Understand whether required weighing and rejection performance remains feasible at the actual sustained rate and pack pitch.

Evidence to compare

Provide sustained and peak rate, actual pack pitch, gap variation, starts, stops and upstream accumulation.

Production condition

shorter available weigh time, unsettled product and transfer disturbance can narrow the usable measurement window.

Acceptance decision

Frame feasibility around representative packs at intended conditions, not a catalogue headline.

The quotation brief should record sustained rate, peak rate and operating profile and pack pitch, gap distribution and weigh-bed occupancy. Final suitability remains specific to the samples, line conditions and acceptance tests agreed for your project.