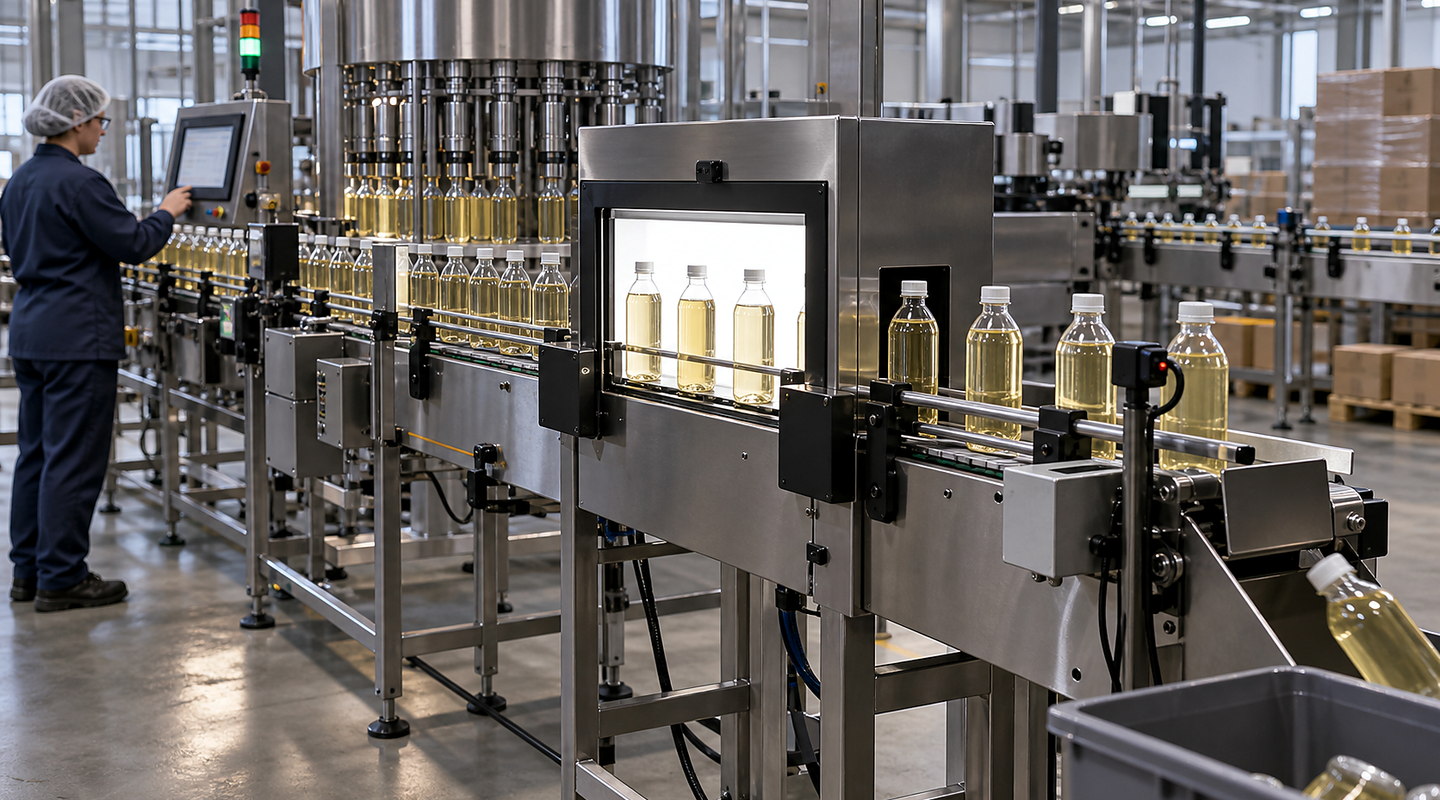
High Speed Checkweighing: How the Process Works
Plan high speed checkweighing trials using pack and tare variation, actual pitch and transfers, known weight challenges, reject tracking, physical removal and recorded acceptance evidence.
Define the pack range, normal product and tare variation and the smallest meaningful weight difference. Trial identified packs at the intended sustained rate, actual pitch and transfer conditions, including vibration and starts/stops where relevant. Follow each failed pack through physical rejection and confirmation, retaining the observed decisions and unresolved limits.
Use the pack stability and spacing record and challenge-test and reject checklist. A rate figure or reject signal alone does not establish usable weighing performance or confirmed removal.
Understand the complete route from input to accepted output — High Speed Checkweighing
Plan high speed checkweighing around the smallest meaningful weight difference, normal product and tare variation, pack transfer, line speed, reject confirmation and traceable test evidence. Follow the material or part through each operating step and include recovery, cleaning and change in the real cycle.
Discuss your application

Four clear stages for high speed checkweighing
At each stage, you can review how pack weight, stability, spacing and normal tare variation at the required rate and test packs, challenge method, records and production response affect the next commitment.
- 01
Measure the Pack, Product and Tare Range
Identify representative pack formats, product and tare variation and known challenge packs. Define the smallest meaningful weight difference, acceptance window and intended production pattern.
- 02
Trial Actual Rate, Pitch, Stability and Transfers
Run the representative range at the agreed sustained rate and actual spacing. Include unstable formats, product movement, conveyor transitions, gap variation and nearby vibration in the recorded conditions.
- 03
Keep Decisions Linked to Physical Rejection
Agree the reject device, removal confirmation, reject-bin state and the line response when a failed pack is not confirmed removed. Keep each pack and its weighing decision associated through the complete sequence.
- 04
Challenge Known Weights and Record Complete Outcomes
Challenge known acceptable, faulty and marginal weights with agreed repetitions, including consecutive rejects and relevant starts/stops. Retain expected and actual weighing/removal outcomes and unresolved follow-up.
Decisions and results stay connected
| Stage | What happens | What you can review |
|---|---|---|
| Measure the Pack, Product and Tare Range | Identify representative pack formats, product and tare variation and known challenge packs. Define the smallest meaningful weight difference, acceptance window and intended production pattern. | Sample/format identities, product/tare range, challenge weights and acceptance requirements. |
| Trial Actual Rate, Pitch, Stability and Transfers | Run the representative range at the agreed sustained rate and actual spacing. Include unstable formats, product movement, conveyor transitions, gap variation and nearby vibration in the recorded conditions. | Actual rate/pitch/gaps, transfers, stability, vibration and trialled operating conditions. |
| Keep Decisions Linked to Physical Rejection | Agree the reject device, removal confirmation, reject-bin state and the line response when a failed pack is not confirmed removed. Keep each pack and its weighing decision associated through the complete sequence. | Pack/result association, physical removal/confirmation and agreed bin/fault responses. |
| Challenge Known Weights and Record Complete Outcomes | Challenge known acceptable, faulty and marginal weights with agreed repetitions, including consecutive rejects and relevant starts/stops. Retain expected and actual weighing/removal outcomes and unresolved follow-up. | Expected/observed results, repetitions, complete-sequence records and unresolved limits. |
Keep connected responsibilities clear
Your final high speed checkweighing scope must also account for reject device, removal confirmation and reject-bin state, test packs, challenge method, records and production response, current regulations and the conditions at your site.
- A checkweigher can only detect a fault that creates a meaningful weight difference.
- Normal product and packaging variation must be understood before setting an acceptance window.
- A reject signal is not proof that the failed pack was physically removed and confirmed.