Current condition
Identify pack formats, product and tare variation, actual sustained/peak rate, pitch and transfers. Record the intended weight decision, acceptance window and how known challenge weights are established.
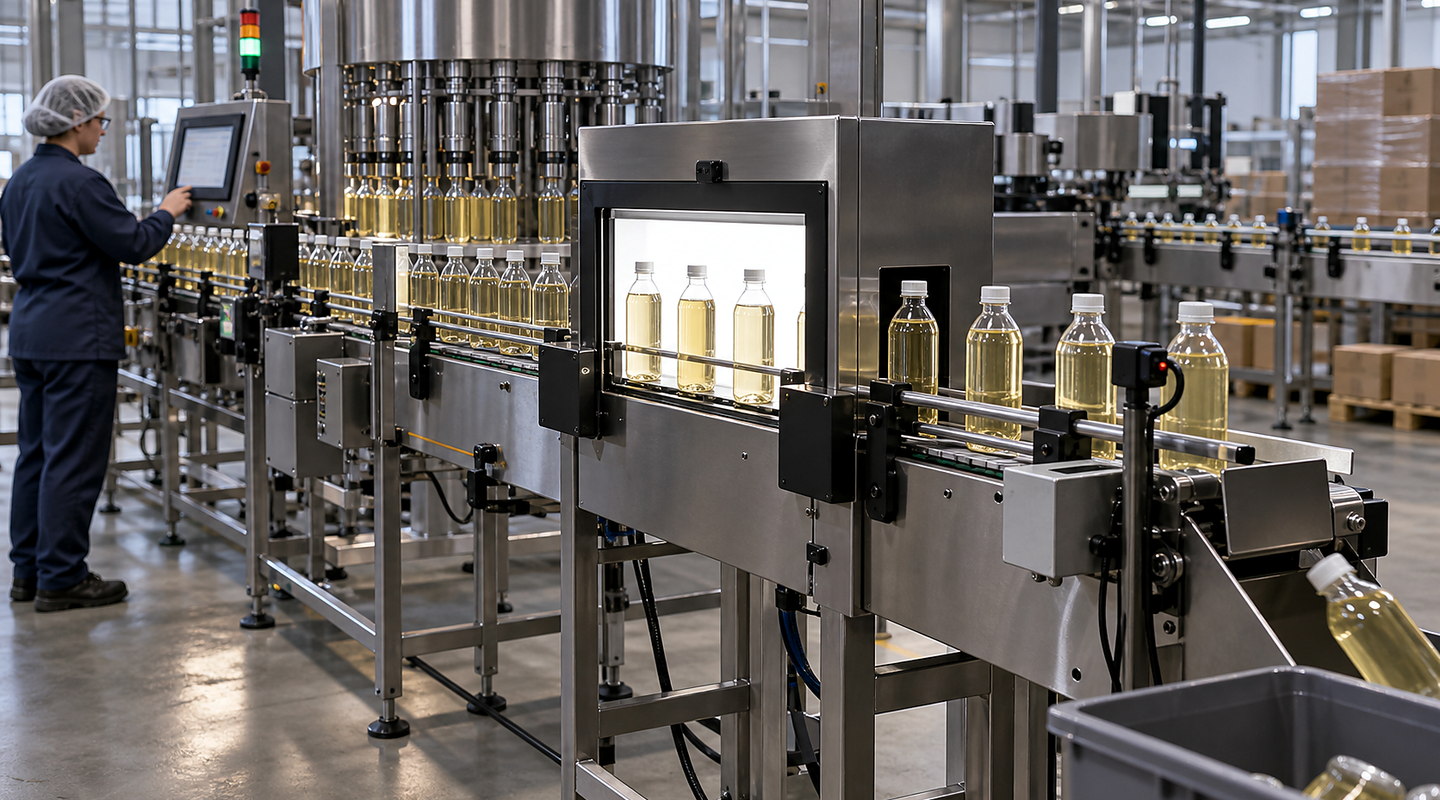
Record high-speed checkweighing pack weights, normal tare variation, stability, actual pitch and gaps, product settling, transfers and vibration with representative challenge results.
Record pack weight, dimensions, normal product and tare variation together with actual rate, pitch and gap distribution. Include unstable formats, product movement, conveyor transitions and nearby vibration. Use these conditions with known challenge packs to test whether the required weight difference remains distinguishable and rejection remains correctly tracked.
Use the complete operating sequence and recorded challenge outcomes. Keep any untrialled pack format, rate or transfer condition explicit rather than extrapolating from one settled sample.
Plan high speed checkweighing around the smallest meaningful weight difference, normal product and tare variation, pack transfer, line speed, reject confirmation and traceable test evidence. Use this guide to resolve pack weight, stability, spacing and normal tare variation at the required rate before it limits the final system.
Discuss your application
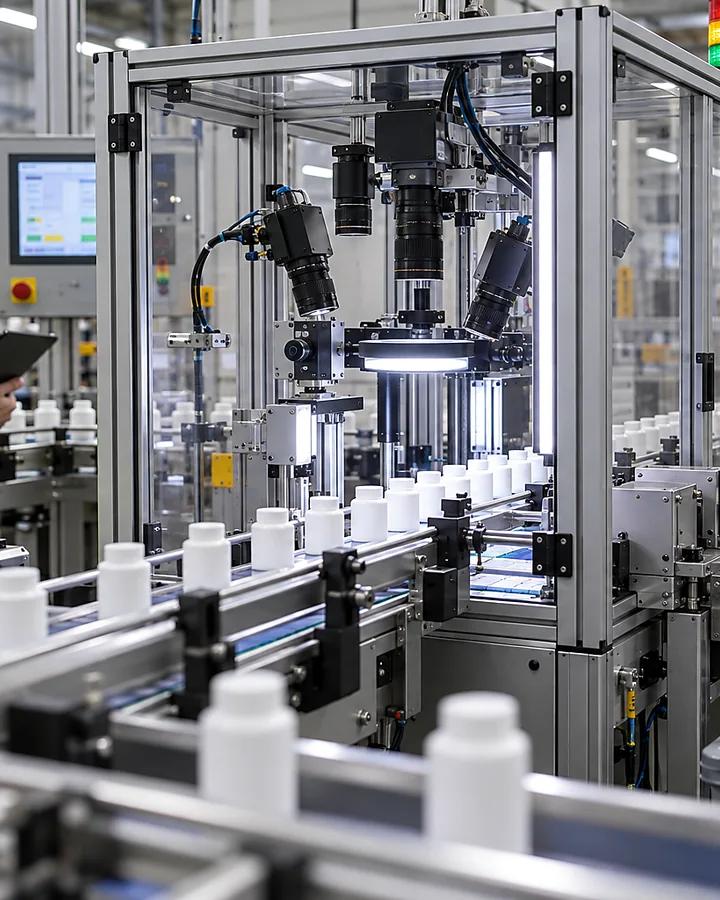
Identify pack formats, product and tare variation, actual sustained/peak rate, pitch and transfers. Record the intended weight decision, acceptance window and how known challenge weights are established.
Include the least stable credible formats, product movement, gap variation, starts/stops and relevant vibration or conveyor transitions. State which formats or running conditions are not covered by the trial.
Record the observed weight decisions, pack tracking, physical rejection and confirmation under those conditions. Agree the line response and owner for uncertain decisions, unconfirmed removal and unresolved trial limits.
Record representative pack weights, normal product and tare variation and the required sustained and peak production pattern. Retain the pack format, stability and spacing conditions alongside each trial result.
Define the smallest weight difference that matters and the intended acceptance window. Compare known challenge packs with normal product and packaging variation before accepting a discrimination claim.
Provide the pack dimensions and least stable credible formats. Observe product movement, pickup onto the weighing conveyor and downstream transfer under the intended running conditions.
Record line rate, actual pack pitch, gap variation, starts/stops, accumulation and nearby vibration. Include acceleration, deceleration and conveyor transitions in the trial conditions rather than citing rate alone.
Keep the failed pack associated with its decision through the reject. Challenge physical removal and confirmation, consecutive rejects and relevant reject-bin conditions, with the required response agreed.
Agree identified test packs, expected decisions, repetitions and records for the complete weighing and reject sequence. Retain actual outcomes, uncertain cases, conditions and responsible follow-up.
Understand whether required weighing and rejection performance remains feasible at the actual sustained rate and pack pitch.
Capture pack mass, length, stability, product movement and gap distribution together.
Include acceleration, deceleration, conveyor transitions and nearby vibration sources.
Use the least stable credible format as a trial case without asserting a maximum rate.
The quotation brief should record pack and product settling behaviour and conveyor transitions, acceleration and vibration. Final suitability remains specific to the samples, line conditions and acceptance tests agreed for your project.